Computer Numerical Control (CNC) machining is widely used to manufacture precision components with complex geometries, tight tolerances, and repeatable quality. While CNC machines provide the physical capability to cut, drill, mill, turn, and shape materials, the machine itself does not decide how a part should be manufactured.
That role is largely performed by CNC programming.
CNC programming creates the instructions that tell a machine tool where to move, how fast to move, which cutting tools to use, how much material to remove, and in what sequence the machining operations should be performed.
Understanding the role of programming is therefore essential to understanding how modern CNC machining works.
What Is CNC Programming?
CNC programming is the process of creating a set of instructions that controls the movement and operation of a CNC machine.
These instructions are commonly represented using G-code and M-code, although modern CNC manufacturing often involves CAD/CAM software that generates much of the machine code automatically.
A CNC program can define parameters such as tool movement, spindle speed, feed rate, cutting depth, coolant operation, tool changes, and machining sequences.
In simple terms, the programming process converts a digital part design into instructions that a CNC machine can execute.
The general workflow can be represented as:
CAD model → CAM programming → Toolpaths → CNC program → Machine operation → Finished part
The quality of each stage can affect the final result.
Why Is Programming Important in CNC Machining?
A CNC machine can provide high positioning accuracy and repeatability, but the machine still needs precise instructions to produce the intended part.
Programming determines how the cutting tool approaches the workpiece and how material is removed. An appropriate program can help achieve dimensional accuracy, efficient material removal, good surface finish, and consistent production.
A poorly developed program, on the other hand, can result in excessive machining time, tool wear, poor surface quality, dimensional errors, or even collisions between the cutting tool and the workpiece or machine.
Programming is therefore not simply a way of telling the machine where to move. It is an important part of the manufacturing engineering process.
From Part Drawing to CNC Program
Before programming begins, the manufacturer normally needs to understand the part design and manufacturing requirements.
A typical CNC machining project may begin with a 3D CAD model and a 2D engineering drawing. The CAD model defines the geometry, while the drawing may specify dimensions, tolerances, surface roughness, material, threads, geometric tolerances, and other requirements.
The programmer then analyzes the component and determines how it can be manufactured efficiently.
This may include deciding:
- Which CNC machine should be used
- Which tools are appropriate
- How the workpiece should be positioned
- Which machining operations are required
- What cutting parameters should be used
- How many setups are necessary
- Which features should be machined first
- How the required tolerances and surface finishes will be achieved
Programming therefore connects part design with actual manufacturing.
The Role of CAM Software
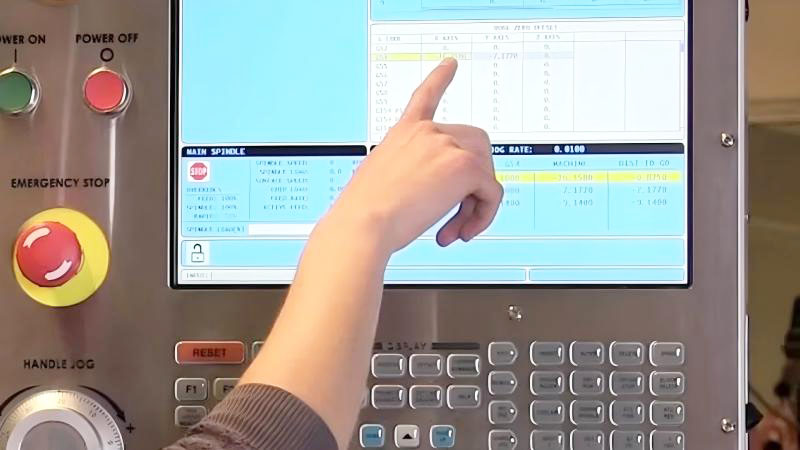
For simple components, CNC programs can sometimes be written manually. However, modern CNC machining increasingly relies on Computer-Aided Manufacturing (CAM) software, especially for complex components.
CAM software uses the CAD model and manufacturing information to generate toolpaths.
A programmer can define the machining strategy and specify parameters such as tool geometry, cutting depth, step-over, feed rate, spindle speed, and machining tolerance. The CAM system then calculates the tool movement required to produce the desired geometry.
The resulting toolpath can be simulated before the program is transferred to the CNC machine.
This is particularly valuable when machining complex parts because it allows potential problems to be identified before actual production begins.
How CNC Programming Controls Tool Movement
One of the fundamental functions of CNC programming is controlling the movement of the cutting tool.
Depending on the machine configuration, the program can control different axes of movement. A typical three-axis machining center uses X, Y, and Z axes, while four-axis and five-axis machines add additional rotary movements.
The program defines coordinates and movement paths that allow the cutting tool to reach specific locations on the workpiece.
For example, a milling program may instruct the machine to move to a particular coordinate, approach a feature, cut along a defined path, retract the tool, and then continue to the next operation.
For complex five-axis machining, programming becomes considerably more sophisticated because the tool orientation can change continuously while the machine moves along multiple axes.
G-Code and M-Code
G-code and M-code are commonly associated with CNC programming.
G-code generally defines machining movements and geometric commands. It can control functions such as rapid positioning, linear interpolation, circular interpolation, and coordinate-related operations.
M-code generally controls machine functions that are not directly related to geometric tool movement. Depending on the CNC controller, these commands can include spindle control, coolant activation, tool changes, and program stops.
The exact syntax and available commands can vary between CNC control systems.
Modern CAM systems often generate these codes automatically through a post-processor configured for a specific machine and controller.
Programming Determines Machining Strategy
One of the most important roles of CNC programming is determining how material will be removed.
The same component can often be machined using different toolpaths and machining strategies.
For example, a milling operation may use roughing to remove large amounts of material quickly, followed by semi-finishing and finishing operations to achieve the required dimensions and surface quality.
A programmer may select different strategies depending on the geometry of the component.
For complex pockets, adaptive or high-efficiency roughing strategies may be used to maintain more consistent cutting conditions. Finishing operations may then follow the contours of the component more precisely.
The objective is not simply to remove material as quickly as possible. The machining strategy must balance productivity, tool life, dimensional accuracy, surface finish, machine capability, and part requirements.
The Relationship Between Programming and Cutting Parameters
CNC programming also determines or incorporates many of the cutting parameters used during machining.
Important parameters include spindle speed, feed rate, depth of cut, and step-over.
These parameters must be selected according to factors such as:
- Workpiece material
- Cutting-tool material and geometry
- Tool diameter
- Machine rigidity
- Spindle capability
- Part geometry
- Required surface finish
- Machining operation
Incorrect parameters can create problems.
Excessive cutting forces may cause tool deflection or premature tool failure. Excessive spindle speed can generate unwanted heat and accelerate tool wear. An unsuitable feed rate can negatively affect surface finish or machining efficiency.
Good CNC programming therefore requires an understanding of both software and machining processes.
Programming and Dimensional Accuracy
Programming has a direct relationship with the dimensional accuracy of a CNC-machined component.
The toolpath determines where the cutting tool travels, while tool geometry, machine accuracy, workholding, material behavior, and cutting conditions also influence the final dimensions.
For high-precision components, programmers may need to compensate for tool diameter, tool wear, machine characteristics, or other process variables.
However, programming alone cannot guarantee dimensional accuracy.
The machine, tooling, workholding, material, inspection process, and manufacturing environment must all work together to achieve the required tolerance.
Programming and Surface Finish
CNC programming also affects the surface finish of machined parts.
Toolpath direction, step-over, feed rate, spindle speed, cutting depth, and tool geometry can all influence the resulting surface texture.
For example, a finishing toolpath with a suitable step-over can reduce visible scallop marks on a contoured surface. Inappropriate toolpath parameters may leave noticeable machining marks even when the component dimensions are correct.
For this reason, a CNC programmer must consider surface-finish requirements during programming rather than treating surface quality as an issue that can always be solved through secondary finishing.
Programming for Complex CNC Machining
As part geometry becomes more complicated, CNC programming becomes increasingly important.
Five-axis machining is a good example.
A five-axis machine can simultaneously control linear and rotary axes, allowing the cutting tool to approach a component from different orientations. This can reduce the number of setups and make it possible to machine features that would be difficult or impossible to access using a conventional three-axis machine.
However, five-axis machining also requires more sophisticated toolpath planning.
The programmer must consider tool orientation, collision avoidance, machine limits, workpiece geometry, holder clearance, and cutting conditions.
This is one reason why advanced CNC programming is closely connected with manufacturing engineering rather than being simply a coding task.
Programming and Production Efficiency
CNC programming has a significant effect on machining efficiency.
An optimized program can reduce unnecessary tool movements, shorten cycle time, improve tool utilization, and reduce the number of machining setups.
For repetitive production, even a small reduction in cycle time can have a meaningful effect on total manufacturing cost.
For example, reducing a machining cycle by 30 seconds may appear insignificant for a single component. If thousands of components are produced, however, the accumulated time savings can become substantial.
Programming efficiency is therefore closely connected to production economics.
Programming for Different Production Volumes
The programming approach can also vary according to production volume.
For a prototype or low-volume project, flexibility may be more important than maximizing cycle-time efficiency. The manufacturer may prioritize quick programming, easy adjustments, and efficient setup.
For larger production runs, greater effort may be invested in optimizing toolpaths, reducing cycle time, extending tool life, and automating repetitive operations.
This is one reason CNC programming should be considered together with the overall production strategy.
The Role of the CNC Programmer Is Changing
Modern CAM software has automated many aspects of CNC programming, but this does not eliminate the need for skilled programmers.
Instead, the role increasingly involves process planning, machining strategy, tool selection, simulation, optimization, and problem solving.
A skilled programmer needs to understand not only how to generate a toolpath but also whether that toolpath is appropriate for the machine, material, tooling, and final part requirements.
In advanced manufacturing environments, CNC programmers may work closely with design engineers, manufacturing engineers, machinists, and quality engineers.
The ability to understand the complete manufacturing process is becoming increasingly important.
CNC Programming and Automation
CNC programming is also an important component of manufacturing automation.
Once a machining process has been properly programmed and validated, the same instructions can be used repeatedly to produce consistent components.
Combined with automated tool changers, probing systems, robotic loading and unloading, pallet systems, and in-process measurement, CNC programming can support highly automated production environments.
This is particularly valuable when manufacturers need to maintain consistent quality across large production quantities.
How to Improve CNC Programming Quality
Good CNC programming begins with a clear understanding of the component and its manufacturing requirements.
The programmer should review the engineering drawing carefully, identify critical dimensions and tolerances, select an appropriate machining sequence, and consider workholding and tool access before creating the final toolpath.
Toolpaths should be simulated and reviewed before production. Cutting parameters should be validated according to the material, tooling, and machine capability.
After machining, inspection results and production feedback can also be used to refine the program.
This creates a continuous relationship between programming and manufacturing:
Design → Programming → Machining → Inspection → Process Improvement
The goal is not simply to create a program that runs. The goal is to create a reliable manufacturing process that consistently produces parts meeting the required specifications.
Conclusion
CNC programming is the link between a digital component design and the physical machining process.
It determines how the cutting tool moves, how material is removed, how machining operations are sequenced, and how the capabilities of the CNC machine are applied to a specific component.
Modern CAM software has made programming faster and more sophisticated, but successful CNC programming still requires knowledge of machining processes, tooling, materials, machine capabilities, tolerances, and quality requirements.
For simple parts, programming may involve relatively straightforward toolpaths. For complex precision components, however, programming becomes an essential part of manufacturing engineering.
Ultimately, the quality of a CNC machine is only one part of the manufacturing equation. A capable machine needs an appropriate machining strategy, and that strategy must be translated into a reliable CNC program.